Within industrial cannery production, the deployment of an automated Heavy-Duty Mechanical Can Clincher and Seamer forms a critical milestone in achieving continuous line efficiency and product uniformity. Integrating this unit into an engineered canned luncheon meat and corned beef processing line demands thorough evaluation of mass flow kinematics, container contact dynamics, and downstream thermal stability.
This technical engineering brief analyzes the mechanical design criteria, operating equations, MEP utility requirements, failure mode diagnostics, and quality validation protocols governing the Heavy-Duty Mechanical Can Clincher and Seamer in modern automated canning lines, with dedicated focus on Mass Flow Kinematics & Sizing (Production Capacity Sizing and Line Balancing).
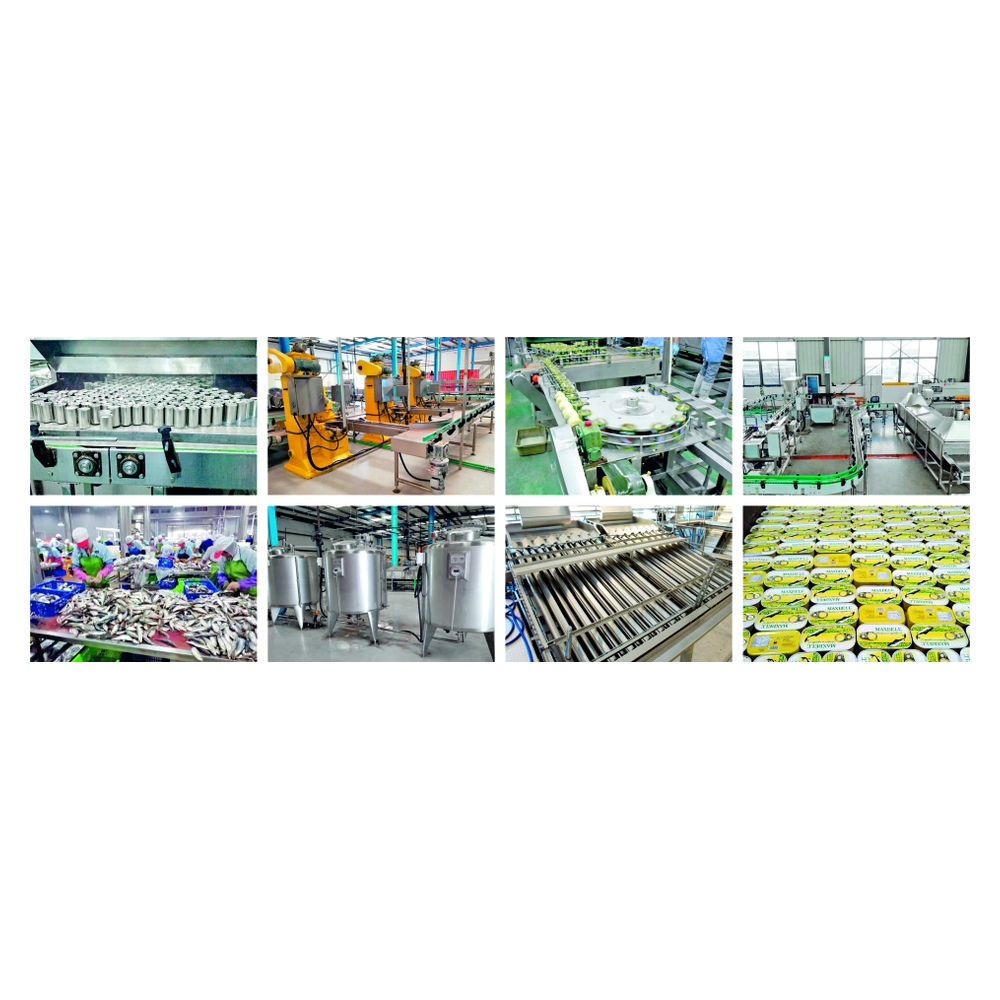
1. Production Capacity Sizing and Dynamic Line Balancing Analysis
Achieving stable high-efficiency output across automated canning lines requires systematic capacity sizing and line balancing for the Heavy-Duty Mechanical Can Clincher and Seamer. When integrating this machinery into the Luncheon Meat & Corned Beef Canning Line, process engineers calculate instantaneous and surge throughput capacities to eliminate upstream accumulation and downstream starvation.
The operational throughput rating is determined by container travel kinetics, machine indexing pitch, and fluid/product transfer velocities. In commercial canneries operating between 60 and 500 cans per minute (cpm), capacity balance is governed by the Mass Flow Rate Equation:
Continuous Cannery Mass Flow Rate Equation:
Q_cpm = (V_belt * 60) / (D_can + S_clearance) * eta_line
Where V_belt is linear transfer speed (m/s), D_can is nominal outer can diameter (m), S_clearance is dynamic inter-can safety gap (0.015-0.030 m), and eta_line is operational efficiency (0.92-0.96).
To prevent line stoppage during downstream seamer tool index changes or retort basket transfers, an integrated accumulation buffer table must provide a minimum of 2.5 to 4.0 minutes of continuous line surge buffering. Dynamic line balancing ensures overall equipment effectiveness (OEE) exceeds 88% across multi-shift production cycles.
2. First and Second Operation Seaming Roll Kinematics
First operation seaming rolls curl the end curl and can body flange into an interlocked seam without metal cutting. Second operation rolls compress the seam under controlled radial load to iron out wrinkles and seat sealing compound.
The structural assembly is constructed from high-tensile sanitary stainless steel, designed to withstand rigorous caustic washdown environments while maintaining precise axis alignment across high-duty operational shifts.
3. Under-Cover Steam Injection and Headspace Deaeration
High-velocity steam jets sweep across the can headspace milliseconds before the cover is placed. As steam condenses post-seaming, it creates a robust internal vacuum of 25 to 45 cmHg, preventing oxidation and lid bulging.
To sustain synchronized production without line starvation, downstream integration is streamlined by connecting with certified water-bath thermal sterilization and heating system systems.
4. Engineering Specifications and Operating Envelope
Factory-calibrated performance parameters for standard and high-throughput industrial operations:
| Engineering Parameter | Standard Operating Baseline | Heavy-Duty Industrial Rating |
|---|---|---|
| Equipment Construction | 4-head rotary mechanical seamer, 120-250 cpm, can diameter 52-99 mm, height 39-160 mm | 6-head high-speed oil-lubricated seamer, 300-500 cpm, titanium-nitride coated rolls, vacuum chamber |
| Primary Electrical Feed | 380V-415V 3-phase, 7.5-15 kW, high-inertia dynamic braking for instant emergency stop (< 0.3s). | Dedicated isolator switch with transient surge suppression |
| Hydraulic & Utility Supply | Steam injection header DN15, 0.2-0.3 MPa dry steam, 45-80 kg/h consumption. | Stainless steel manifold with sanitary isolation valves |
Foundation specifications require a reinforced concrete slab (minimum C30/37 structural grade) equipped with high-density anti-vibration elastomeric isolation mounts, isolating dynamic cyclic harmonics from adjacent cannery floor cells. The machine operating envelope supports continuous processing in ambient temperatures from +5 deg C to +45 deg C with relative humidity up to 95% non-condensing. All on-board control enclosures are rated to IP69K stainless construction with active internal vortex cooling manifolds to prevent moisture condensation during intensive high-pressure washdown shifts.
5. Engineering Principle & Analytical Sizing Model
Process modeling and capacity calculation adhere to verified thermodynamic and kinetic equations:
Double Seam Percentage Overlap Equation:
Overlap % = [Body Hook (mm) + Cover Hook (mm) + End Plate Thickness (mm) - Seam Length (mm)] / [Seam Length - (2*EPT + 3*BPT)] * 100%
Practical Calculation: For a standard 300x407 tinplate can: BH = 1.48 mm, CH = 1.52 mm, EPT = 0.22 mm, BPT = 0.20 mm, Seam Length = 3.05 mm: Net Overlap = 1.17 mm (Overlap ratio = 62.5%, well exceeding the 55% international safety minimum).
Adhering to this mathematical model allows project engineers to accurately size upstream batch buffers and downstream conveyance without risking product accumulation or thermal degradation. Finite element stress simulations (FEA) and computational fluid dynamics (CFD) validate that mechanical deflections remain under 0.015 mm under peak line surges, preserving continuous mass-balance equilibrium and preventing container deformation during high-speed transfer operations.
6. Failure Mode and Effects Diagnostics (FMEA)
Critical operational fault signatures, root-cause pathways, and field remediation actions:
| Operational Fault Signature | Probable Root Cause | Field Corrective Action |
|---|---|---|
| False Seam (Disengaged Hooks) | Severely damaged can flange; misaligned cover feed; seaming chuck lip chipped | Inspect empty can flange integrity; align cover separator knives; replace damaged carbide seaming chuck. |
| Cutover (Sharp Metal Crest at Chuck Rim) | Excessive second operation roll pressure; worn seaming chuck contour radius | Back off 2nd operation roll adjusting screw by 0.05 mm; verify chuck lip radius using optical gauge. |
| Loose Seam / Low Tightness (< 70%) | Worn roll pin bearings; base plate lifter spring tension below required 85 kgf | Replace roll pin needle bearings; measure lifter spring preload using calibrated force gauge. |
7. Preventative Maintenance and Commissioning Spares Strategy
To preserve line efficiency and achieve planned preventative maintenance objectives:
- Daily Inspection Protocol: Clean product-contact zones with neutral detergent; inspect pneumatic seals and line strainers; record operating pressures.
- Monthly Lubrication & Calibration: Replenish NSF H1 food-grade grease in sealed bearing housings; calibrate sensor switching thresholds; check drive chain tension.
- Critical Spares Kit on Hand: Maintain on-site: 2 complete sets of TiN-coated 1st and 2nd operation seaming rolls, 2 seaming chucks, 4 lifter spindle springs.
- Annual Overhaul & Dynamic Laser Alignment: Perform precision laser shaft alignment and dial-indicator spindle runout verification (maintaining total radial deflection strictly under 0.025 mm). Execute acoustic vibration spectral FFT analysis per ISO 10816-3 Class II industrial standards to detect early bearing raceway micro-spalling before catastrophic fatigue occurs.
For end-of-line secondary handling and packing automation, explore our complementary continuous canned fish brine draining and oil dosing unit.
8. Sanitary Hygiene Engineering & Regulatory Compliance Protocols
Industrial canning lines must comply with rigorous international food safety standards, including FDA 21 CFR Part 113 for low-acid canned foods, European EHEDG guidelines, and 3-A Sanitary Standards. Contact parts manufactured from AISI 316L stainless steel undergo electrolytic polishing to achieve surface finishes below Ra 0.8 micrometers, eliminating microscopic crevices that harbor bacterial biofilm.
Automated Clean-in-Place (CIP) and Steam-in-Place (SIP) routines are integrated directly into the machine control architecture. Automated sequencing controls deliver a 5-stage cleaning cycle: initial warm water pre-rinse, circulating caustic wash (1.5-2.0% NaOH at 75-85 deg C) with turbulent flow velocities exceeding 1.5 m/s, intermediate potable water rinse, nitric acid neutralization flush (0.8-1.2% HNO3 at 60 deg C) to remove mineral scale, and final cold sanitizing rinse. Digital conductivity probes and flow transmitters continuously verify chemical concentration and turbulent velocity, generating encrypted audit logs required for third-party BRCGS and IFS Food safety certifications.
Every unit supplied by HSYL undergoes exhaustive Factory Acceptance Testing (FAT) before shipment. Verification packages include full Installation Qualification (IQ) and Operational Qualification (OQ) protocols, material test reports (EN 10204 3.1 certification), weld inspection records, and calibrated thermal and dimensional validation certificates ensuring immediate, compliant commissioning on the cannery plant floor.
Related Articles


Get professional consultation
Do you have any questions or need technical support regarding the content of this article? Fill out the form below, and our expert team will provide you with professional solutions.