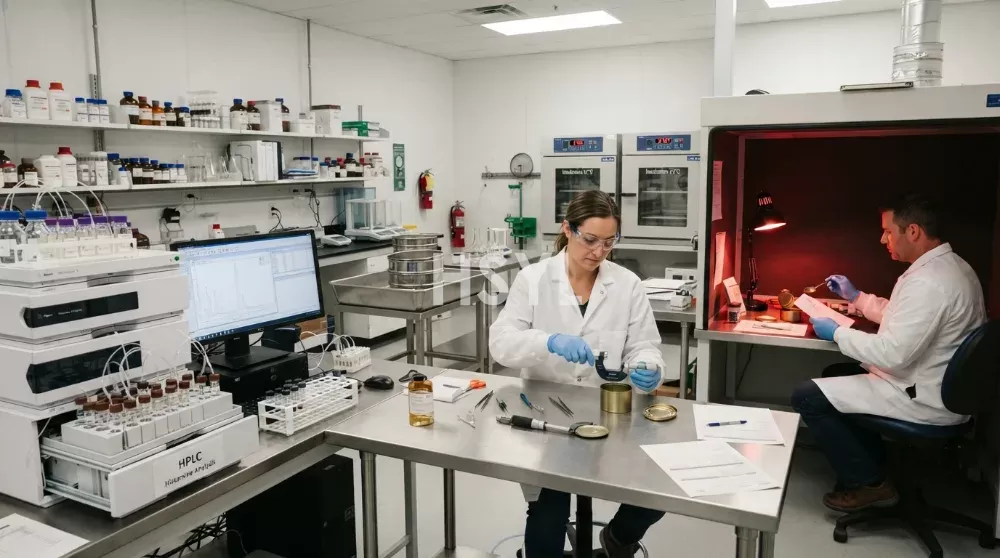
Sardine and Mackerel Canning: Small Pelagic Fish Processing Line
A sardine and mackerel canning line processes small pelagic fish — typically 10–...


Tuna canning production line for low-acid seafood: pre-cooking, loin cleaning, filling, vacuum seaming and retort sterilization. Request a turnkey quote.
| Configuration | Reference Capacity | Automation | Typical Buyer |
|---|---|---|---|
| Pilot / small scale | 1,500-2,500 cans/hr | Semi-automatic | Startups, regional canneries |
| Mid scale | 8,000 cans/hr | Fully automatic | Export-oriented processors |
| Turnkey plant | 20,000+ cans/day | Fully automatic with utilities | New factory projects |
For complete autoclave batch scheduling and facility sanitation planning, refer to our engineering overview on retort sterilization is crucial.
Detailed model parameters (power, footprint, steam consumption) are confirmed on the model specification sheet against your product and can format.
A tuna canning project starts with the incoming raw material. Processing whole tuna requires a different preparation section from a plant receiving cleaned, pre-cooked loins. Define this starting point before comparing equipment capacity, factory space or investment.
HSYL configures tuna canning projects around the required product style, can format and output. The quotation should identify the preparation equipment, tuna filling system, liquid dosing, can seaming, retort section and downstream handling included in the supply. Existing equipment and manual operations should also be recorded so that the proposed line matches the actual factory workflow.
| Specification Parameter | Technical Data |
|---|---|
| Model Configuration | HSYL-TC150 Turnkey Line |
| Production Capacity | 80 - 150 cans / min (Adjustable via VFD) |
| Applicable Containers | Tinplate, Aluminum, Easy-Open Ends (EOE), Club Cans |
| Total Installed Power | Approx. 135 kW |
| Standard Power Supply | 380V / 50Hz / 3 Phase (Customizable) |
| Steam Consumption | 1800 - 2200 kg / h (Operational pressure: 0.6 - 0.8 MPa) |
| Compressed Air Requirement | 0.6 MPa / 3.5 m3 / min |
| Line Footprint (L x W x H) | Approx. 35,000 mm x 5,000 mm x 3,200 mm |
| Core Material Grade | SUS304 Frame / SUS316L Fluid Contact Parts |
For a conventional pre-cooked whole-fish route, preparation includes receiving, thawing where required, fish preparation, pre-cooking, cooling and loin cleaning before packing. The species, fish size and intended product style influence the preparation arrangement.
A plant receiving cleaned, pre-cooked tuna loins has a different starting point. Its equipment scope should reflect the condition of the supplied loins and the handling needed before filling. It should not automatically duplicate the whole-fish cooking and cleaning section.
State whether the finished product will be solid pack, chunks, flakes or another style. This helps define the filling method and the texture to preserve.
Histamine control begins with raw-material sourcing and handling. Equipment layout can help reduce unnecessary waiting, but rapid conveying or retort sterilization cannot correct fish in which histamine has already formed.
Receiving controls, time and temperature management, testing and corrective actions should follow the processor's hazard analysis and applicable market requirements. The equipment proposal should support those controls without presenting the machinery itself as a guarantee of food safety.
The tuna filler should be selected for the product style, can dimensions and agreed fill requirements. Liquid dosing must accommodate the selected oil, brine or sauce. Net weight and drained weight should have separate acceptance criteria; they should not be treated as interchangeable measurements.
Can and end compatibility, seaming tooling and seam inspection requirements must be confirmed for the proposed containers. Vacuum arrangements should be specified for the product and process rather than presented as a substitute for double-seam control.
The thermal process must be established by a qualified processing authority for the relevant product, container and processing system. A single retort temperature or generic cycle time does not define an adequate process for every canned tuna recipe.
Compare quotations using the same can format, product style and operating schedule. Distinguish the rated speed of an individual filler or seamer from the finished output of the complete line.
Retort sizing should account for basket capacity, loading, the established processing cycle, cooling and unloading. Include preparation capacity, operator tasks and downstream packing when assessing whether the proposed system can sustain the required output.
Inspection equipment should be identified by the defects it is intended and demonstrated to detect. Checkweighing, foreign-body inspection and seam examination serve different purposes; one inspection device should not be assumed to verify every aspect of can integrity.
Develop the layout around raw-material handling, preparation, filling and seaming, retort operations and finished-can handling. Review personnel routes, waste removal, drainage and access for cleaning and maintenance.
Confirm steam, water, compressed air and electrical demand against the final equipment list. Identify whether boilers, water treatment, cooling systems, utility pipework and installation are included or supplied separately.
Request the equipment specifications, layout, utility schedule, operating manuals, cleaning instructions, spare-parts recommendations and commissioning scope.
Cleaning methods must match the documented protection and construction of each component. An enclosure IP rating alone does not establish suitability for whole-line high-pressure chemical washing.
Equipment documentation and factory acceptance testing support project implementation. They do not replace the processor's process validation, operating controls or destination-market obligations.
Provide the incoming tuna form, species and size range; finished product style; can and end specifications; filling medium; target output; working hours; and available factory layout.
Ask for a quotation that separates preparation, filling, seaming, retorts, handling, inspection, utilities and installation. This makes both the investment and the responsibilities easier to compare.
Review the canned food production line overview for other canning applications and equipment categories.


A sardine and mackerel canning line processes small pelagic fish — typically 10–...
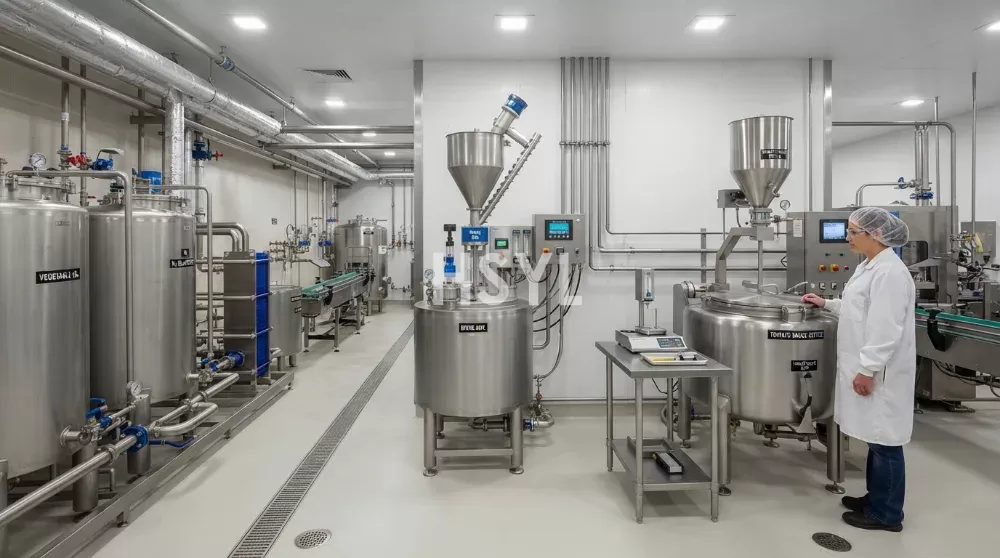
The filling medium — the liquid that fills the void spaces between the fish piec...
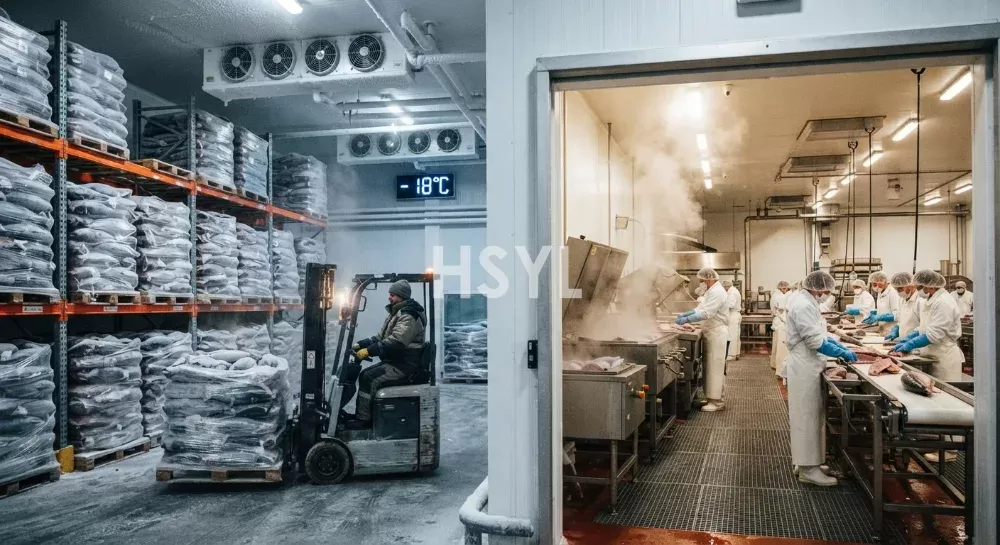
Direct AnswerThe most expensive asset in a fish cannery is not the retort or the...
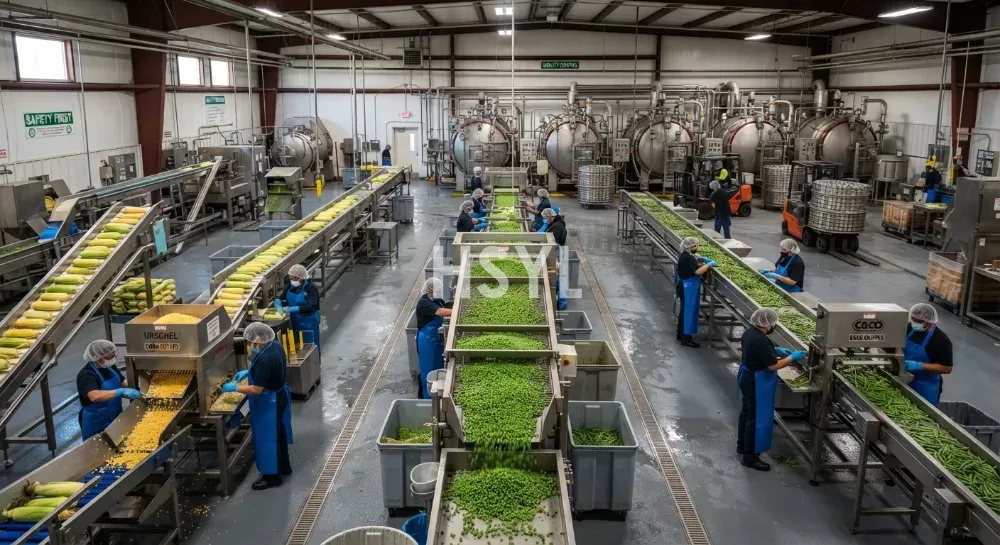
Direct AnswerA low-acid canned vegetable processing line — corn, peas, and green...