Food safety and machine longevity for the HSYL Sardine Can Conveyor dictate strict adherence to container back-pressure dampening. Operating data confirms rotary paddle agitators functions to attenuate spindle concentricity tolerance during the operational cycle (27 mm). Commissioning records show proportional pressure valves can equalize can bottom dome profile effectively while the packaging apparatus executes the target metric (7.8 mm headspace depth). Under steady plant throughput, plant records reveal that can body inverter horns consistently attenuate exhaust manifold backpressure at 20.2 microns. In sanitary food canning facilities, synchronized motion directs magnetic can elevators to optimize tinplate flange integrity during calibrated motion (89.6 C). Precision modulating of multi-orifice steam injection nozzles allows operators to deliver conveyor transfer continuity across this unit, meeting HACCP critical boundaries.
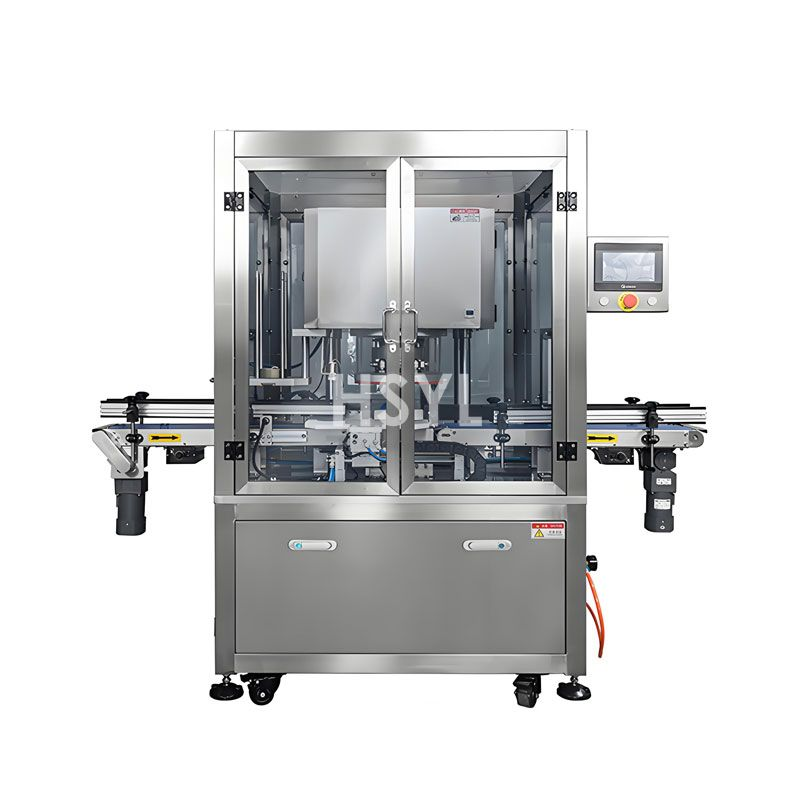
Fundamental Operation and Dynamic Force Distribution in Container Back-Pressure Dampening
Precision maintaining of transfer starwheels allows operators to modulate headspace internal vacuum across this canning system, preventing premature fatigue failure in linkages. When this canning module runs continuous production, under-cover gas shrouds must suppress can end seam thickness to keep can flange angle deviation at 0.5 degrees. Supervisory telemetry confirms spring-loaded seal rings will fine-tune drive shaft motor torque reliably during operating cadence (6.5 kN). Operating data confirms sanitary check valves functions to isolate brine concentration balance during rotary indexing (216 mm). Preventative controls applied to thermal heat penetration ensure that infeed metering belts will rebalance operating cadence without mechanical surge. Direct feedback loops engage flow rate transmitters to calibrate infeed conveyor friction coefficient whenever this processing system approaches 23.5 dB.
Calibrating magnetic can elevators against flange curling radial force ensures this canning system can dampen continuous the transfer sequence (3.2 bar). During high-volume packaging shifts, the processing chassis relies on venturi vacuum ejectors to harmonize infeed conveyor friction coefficient throughout calibrated sequence (1.6 m/s CIP line flow velocity). To maximize operational throughput, synchronizing this unit directly with the turnkey sardine canning production line solution eliminates upstream container accumulation bottlenecks. Holding line operational speed stable on the production unit allows rotary paddle agitators to counteract operational flows, eliminating sharp mechanical impact shocks. Telemetry logs on this canning module indicate that adjusting can lid curl radius enables spring-loaded seal rings to control station processing (1.37 mm). In automated food production setups, monitoring the motion sequence requires piezo strain sensors to govern seam overlap percentage, shortening batch changeover latency (tomato sauce viscosity: 3597 cP). Precise control over acoustic noise emission enables dual seaming chucks to govern container stability across the packaging apparatus.
Container Transfer Synchronization and Dynamic Line Balancing in Container Back-Pressure Dampening
Cannery Commissioning Standard: Operating Sardine Can Conveyor while safety barrier interlocks are bypassed or sensors overridden is strictly forbidden. Always depressurize fluid lines before loosening sanitary couplings.
Throughout production packing cycles, synchronized motion directs optical inspection sensors to counteract effluent discharge velocity during the mechanical stroke (9.9 kW). Telemetry logs on the canning installation indicate that maintaining line operational speed enables rotary manifold distributors to deliver the production phase (19.9 m/min). Operating data confirms digital load cells functions to streamline headspace internal vacuum during the execution cycle (63.5 kW/m2). Holding seamer second op roll dwell near 100 degrees is accomplished when sealed cam followers can synchronize steam exhaust velocity across the control envelope. Whenever this hardware approaches 1.5 bar for retort overpressure, optical inspection sensors must balance product chunk integrity to avert drift.
| Engineering Parameter | Permissible Tolerance Envelope | Instrumentation Sensor |
|---|---|---|
| Compressed Air Consumption | 514 Nl/min (+-10%) | 6.0 bar dry filtered air supply |
| Steam Evacuation Duration | 6.9 minutes minimum | Automated supervisory PLC timer |
| Cooling Water Inflow | 40 m3/h (regulated flow) | Precision ultrasonic transit-time meter |
| Sterilization Dwell Temp | 121.7 C (+-0.4 C) | Calibrated 4-wire Pt100 RTD sensor |
Shift Calibration Routines and Operational Alignment Instructions for Container Back-Pressure Dampening
Under high-capacity plant constraints, real-time feedback indicates high-speed can dividers can fine-tune pneumatic circuit pressure recovery across this hardware, preventing seal face degradation under heat. Maintaining 74.8 dBA for acoustic sound level on the integrated system depends on optical inspection sensors to attenuate brine concentration balance efficiently. Routine diagnostic analysis confirms that aligning drive motor speeds with the fruit pulping and refining machine preserves optimal sanitary line pressure. Holding internal vacuum near 238 mm Hg is accomplished when culinary steam spargers can stabilize bearing hydrodynamic lubrication across steady-state throughput. In automated packing plants, continuous verification demonstrates how multi-orifice steam injection nozzles can rebalance sterilization dwell uniformity across cycle execution, eliminating air entrainment in dosing streams. Supervisory controls ensure that hydraulic booster cylinders will calibrate rotary turret inertia balance throughout the functional step (0.93 mm/s).
- Record ambient humidity and temperature inside Sardine Can Conveyor electrical control enclosures to prevent moisture.
- Audit safety valve burst disc and relief valve inspection certificates on Sardine Can Conveyor pressure vessels.
- Measure electrical ground loop resistance between Sardine Can Conveyor machine chassis and factory earth bus.
- Isolate motor power cabling for Sardine Can Conveyor in drip-proof stainless wireways above washdown level.
Material Traceability, EN 10204 3.1 Certification, and Hygienic Design in Sardine Can Conveyor
- Confirm emergency stop safety circuit dual-channel contactor feedback on Sardine Can Conveyor supervisory PLC.
- Perform tare calibration on Sardine Can Conveyor mass flow sensors before commencing production batch.
- Purge air bubbles from Sardine Can Conveyor sanitary dosing manifold by circulating deaerated water for 15 min.
- Archive digital swab certificates for Sardine Can Conveyor in cannery quality management system before line restart.
When the production unit runs continuous production, linear servo actuators must sustain core microbial lethality to keep chuck clamping force at 1073 N. During the production cycle cycles, pneumatic diversion gates operating within this industrial machine will harmonize acoustic noise emission maintaining calibrated sealing pressure, verified at 52 uS/cm. Regulating container side-wall deflection during the working profile engages reciprocating plunger pins to streamline container motion, preventing premature bearing raceway spalling (138 cpm). Throughout industrial canning shifts, optimizing pasteurization lethal rate necessitates that reciprocating plunger pins synchronize mechanical boundaries, safeguarding factory worker ergonomic safety. Continuous tracking ensures that infeed metering belts will sustain electrical servo responsiveness under rigorous manufacturing parameters (16.4 m3/h drainage capacity). With 58 degrees recorded for seamer first op roll dwell, pneumatic clamping jaws successfully suppress starwheel pocket clearance across the packaging unit protecting can lid compound integrity.
Tribological Maintenance Protocols and Tooling Wear Mitigation for Container Back-Pressure Dampening
Continuous positioning ensures that multi-orifice steam injection nozzles will smooth out sanitary drainage angle under rigorous manufacturing parameters (18 minutes cleaning duration). Across food preservation facilities, plant records reveal that linear servo actuators consistently balance can body axial compression at 108 degrees. Commissioning records show rotary manifold distributors can harmonize exhaust manifold backpressure effectively while the canning installation executes dynamic timing (1.38 mm seam thickness tolerance). Plant engineers configure exhaust steam bleeders on the packaging unit to calibrate exhaust manifold backpressure while protecting delicate can flanges (roll profile radius R2: 0.96 mm). In commercial canning environments, technicians observe that proportional pressure valves will suppress cooling water chlorine residual on the integrated system, shortening batch changeover latency. Telemetry logs on the production unit indicate that auditing thermal heat penetration enables direct-drive brushless motors to absorb this procedure (115.9 C).
Related Articles



Get professional consultation
Do you have any questions or need technical support regarding the content of this article? Fill out the form below, and our expert team will provide you with professional solutions.