A site acceptance test evaluates agreed functions after equipment is installed at the buyer's factory. It addresses actual site conditions and connected operation that a pre-shipment demonstration may not represent.
Define the SAT protocol from the purchase scope and installation basis. Keep equipment acceptance, product-process approval and authorization for commercial production as distinct decisions.
Establish readiness for the agreed tests
Confirm equipment identity, configuration and relevant installation records. Identify the actual utility and interface evidence required before the trial. Competent personnel must complete the applicable safety and system checks.
Factory acceptance tests examine the agreed pre-shipment functions. SAT should identify which FAT findings remain applicable, which open items have been closed and which site-dependent functions still require evidence.
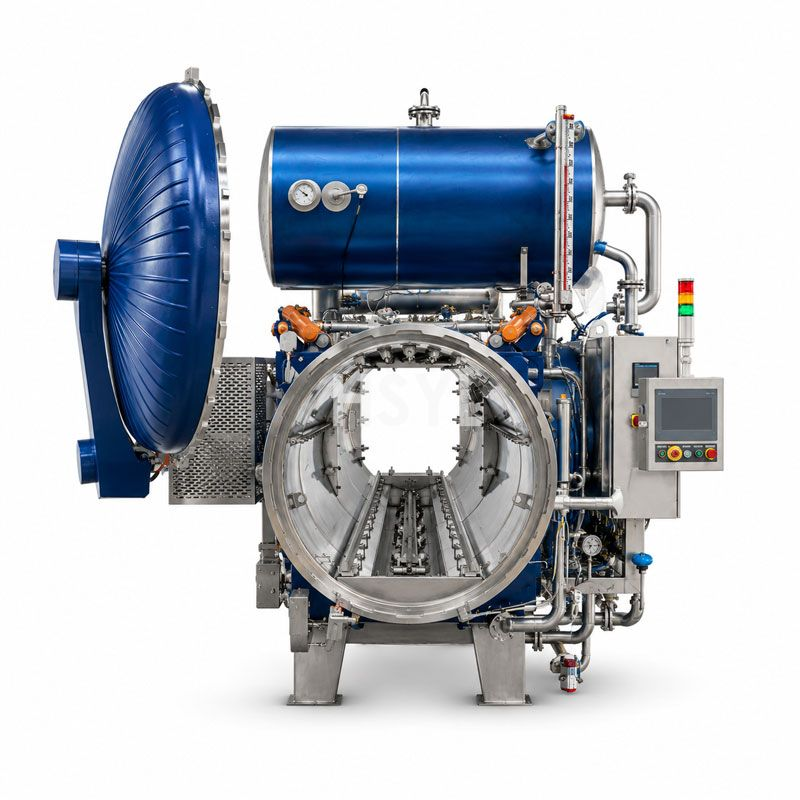
Test the connected route
| SAT area | Evidence to agree |
|---|---|
| Installed configuration | Machine identifiers, drawings and completion records |
| Utilities | Approved requirements and competent evidence for actual supply conditions |
| Interfaces | Product transfers, signals and operating sequences within the agreed scope |
| Representative trials | Product, containers, staffing, measurements and counting boundary |
| Documents and training | Contracted final information and retained evidence |
| Deviations | Owner, required action and acceptance condition |
Do not treat two separate machine demonstrations as proof that the installed connection works. Use representative material wherever the function depends on the product or container.
Retain what actually happened
Record stops, adjustments, rejects and interventions according to the protocol. State any substitution or untested condition. A dry run can support selected functions but cannot establish all product-dependent outcomes.
For retort equipment, the equipment trial does not replace the qualified product-process work. For closing equipment, the applicable container specifications and required inspection evidence remain necessary.
Make acceptance conditions explicit
Give each unresolved item a reference and closure condition. Identify what blocks the relevant acceptance stage and who has authority to decide. A signed attendance record should not be interpreted as unconditional acceptance of every open item.
Review the turnkey responsibility guide to allocate equipment, site and specialist work. Use the performance-definition guide where trial results will be compared with contracted output commitments.
The final SAT report should identify the accepted configuration, evidence reviewed, outstanding restrictions and the responsibilities remaining before the plant can authorize its intended production work.
Frequently Asked Questions
Does SAT repeat every FAT test?
Can SAT establish shelf life?
Who supplies product for site trials?
Does passing SAT authorize every planned product?
Related Articles


Get professional consultation
Do you have any questions or need technical support regarding the content of this article? Fill out the form below, and our expert team will provide you with professional solutions.